Bin Robot System
Autonomous bin robots handle storage, retrieval, and internal transport of materials across the warehouse floor with high precision
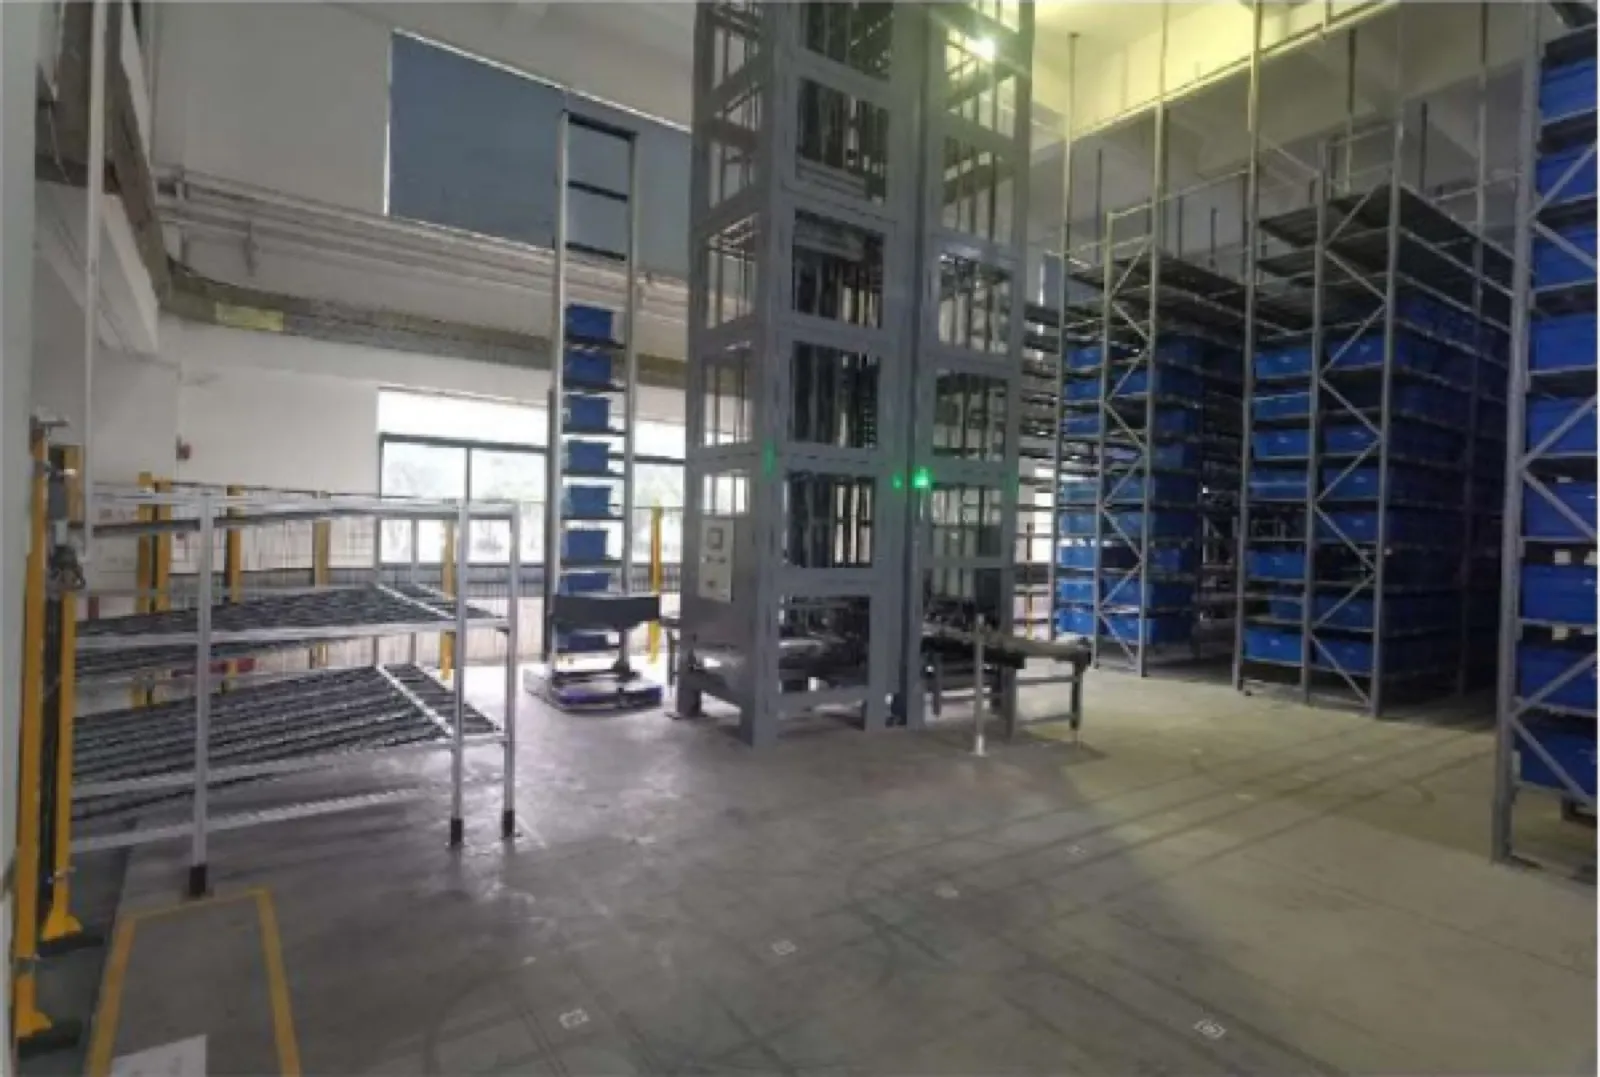
Bin robots + conveyors + lifters: seamless multi-floor logistics for residential building products
Building Materials · Multi-Floor · Bin Robot + Conveyor · WMS/WCS
Seagull Housing Industry, listed on the Shenzhen Stock Exchange, is a leading manufacturer of residential building products including bathroom fixtures, kitchen systems, and prefabricated interior components. With a diversified product portfolio spanning multiple categories and production lines spread across different floors, Seagull faced growing complexity in internal material handling and warehouse operations.
The operating constraints Seagull brought to the project.
Multi-floor production facility requiring frequent cross-floor material transport between storage and production lines
Diverse product categories (bathroom, kitchen, prefab components) with varying storage requirements
Manual material handling causing bottlenecks and delays in production scheduling
Limited visibility into real-time inventory levels across multiple floors and zones — a pain point also solved for Comix in their office supplies warehouse
Need for a flexible system that can adapt to changing production demands and seasonal peaks
System components delivered for Seagull, orchestrated by our WES.
Explore the HardwareAutonomous bin robots handle storage, retrieval, and internal transport of materials across the warehouse floor with high precision
Automated conveyor lines and vertical lifters connect multiple floors, enabling seamless cross-floor material flow without manual intervention
Warehouse Management System and Warehouse Control System provide real-time inventory tracking, task scheduling, and system coordination across all floors
Modular system design allows easy scaling — add more robots or extend conveyor lines as production demands grow
Direct connection between automated warehouse and production lines ensures just-in-time material delivery to workstations
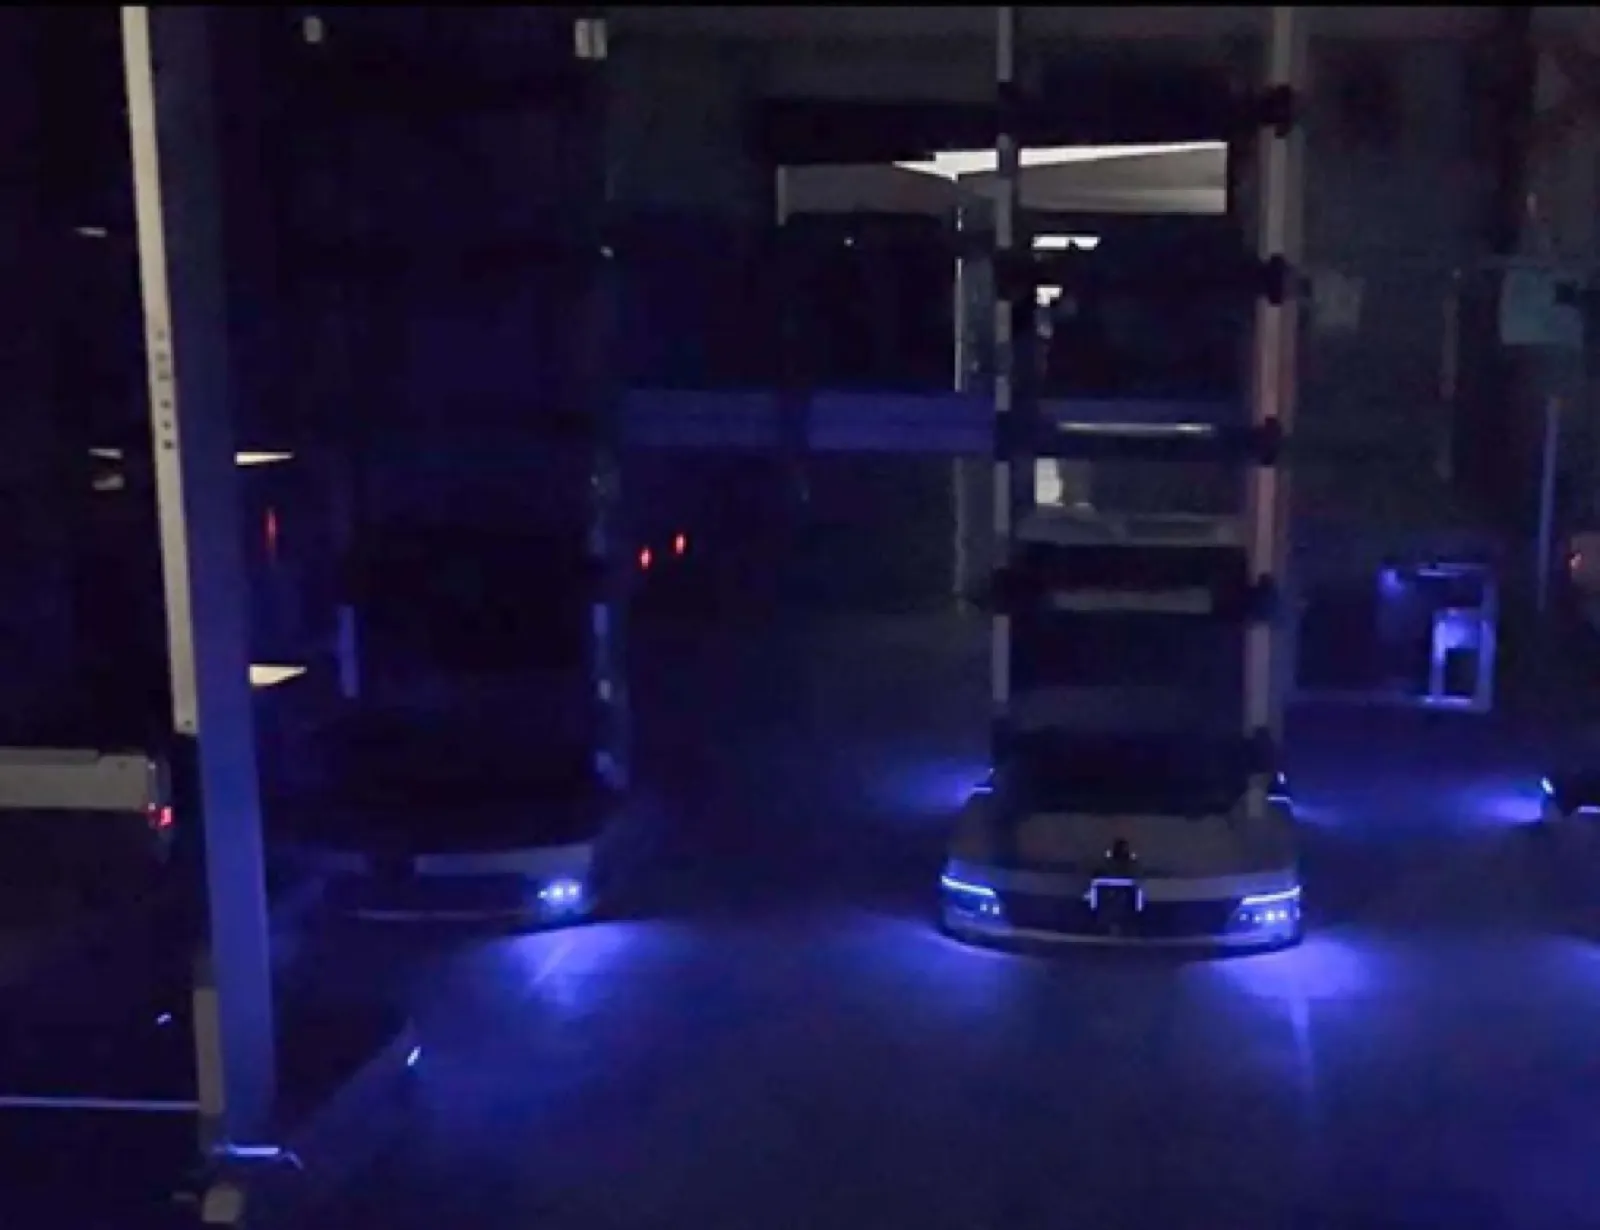
Photos from the Seagull project.
In the manufacturing sector, YKK achieved fully unmanned 24/7 operation using a similar goods-to-person approach with bin robots and robotic arms for their fastener warehouse.
Get a Similar AssessmentMoving materials horizontally is a solved problem. Moving them vertically between production floors — continuously, automatically, and without bottlenecks — is where most automation projects stall.
Single-story warehouses dominate the automation landscape for a reason: flat floors are simple. Robots roll, conveyors run, and the entire operation exists on one plane. Multi-story facilities like Seagull's break that assumption.
Seagull's building materials production spans multiple floors, each dedicated to different manufacturing stages. Raw materials enter at ground level, processing happens on intermediate floors, and finished goods stage for shipping from upper levels. The material flow crosses floor boundaries dozens of times per hour.
Before automation, this vertical movement relied on freight elevators operated by dedicated staff. Elevators are batch processors — they accumulate a load, travel, unload, and return. During peak production, elevator wait times became the constraint that limited the entire facility's throughput. Adding more elevators was not feasible without major structural modifications to the building.
Seagull's solution combines three automation technologies that each handle one dimension of the logistics problem. Tote robots manage horizontal movement within each floor — retrieving materials from storage, delivering to workstations, and collecting finished goods. Conveyor lines connect robot zones to the vertical transport points. Dedicated lifters move totes between floors on continuous cycles rather than batch elevator runs.
The WES orchestrates all three systems as a single material flow. A production order triggers a retrieval task on floor one, routes the tote to a conveyor feeding the lifter, raises it to floor three, and hands it off to a robot on that floor for delivery to the target workstation. The entire sequence runs without human intervention and without the tote waiting in a queue for an elevator.
In our experience, the lifter integration is where multi-story projects succeed or fail. Lifters must cycle continuously at speeds that match the horizontal throughput on each floor. If the lifter is slower than the robot fleet feeding it, totes queue up and the bottleneck simply moves from the old elevator to the new lifter. We sized Seagull's lifter capacity at 120% of peak horizontal throughput to maintain buffer headroom.
Building materials present handling challenges that consumer goods do not. Components are heavy — ceramic fixtures, metal fittings, glass panels — and often irregularly shaped. The hardware systems deployed at Seagull use reinforced totes with adjustable compartments and robots rated for loads well above the standard tote-robot capacity used in e-commerce fulfillment.
The weight factor compounds in vertical transport. A lifter moving heavy totes between floors operates under structural loads that require engineering analysis of the building itself — floor load ratings, shaft reinforcement, and vibration isolation to prevent lifter operation from affecting manufacturing processes on adjacent floors.
For manufacturers operating in multi-story facilities, the solutions page covers how we assess vertical logistics requirements. The types of ASRS systems guide explains which storage architectures work within floor-height constraints. The goods-to-person picking approach adapts to multi-floor layouts with station placement on each level.
Questions we hear about projects like Seagull.
Ask our engineersThe WES assigns priority based on production schedule urgency, not floor number. A time-critical material request from floor four jumps ahead of a routine replenishment task from floor two. During peak periods when all floors generate high demand simultaneously, the system switches to a round-robin allocation with priority overrides — each floor gets guaranteed minimum lifter cycles per hour, with surplus capacity allocated dynamically. The cost analysis page factors in lifter sizing and redundancy when modeling multi-story automation investments.
The lifter shaft is the primary structural requirement — a vertical channel with reinforced walls, load-bearing capacity for the lifter mechanism plus maximum tote weight, and vibration isolation. Floor penetrations for conveyor connections between levels are smaller but require fire-rating compliance. Seagull's installation required structural engineering review but no major building modifications because the lifter shaft used an existing utility chase. Contact our team with your building specifications for a feasibility assessment.
Yes, with constraints. The building needs sufficient floor load capacity for robot traffic, ceiling height for racking on each floor, and a viable path for the lifter shaft. Older industrial buildings often meet these requirements because they were built for heavy manufacturing loads. The mini-load ASRS guide covers compact storage options that work within the tighter ceiling heights common in multi-story facilities.
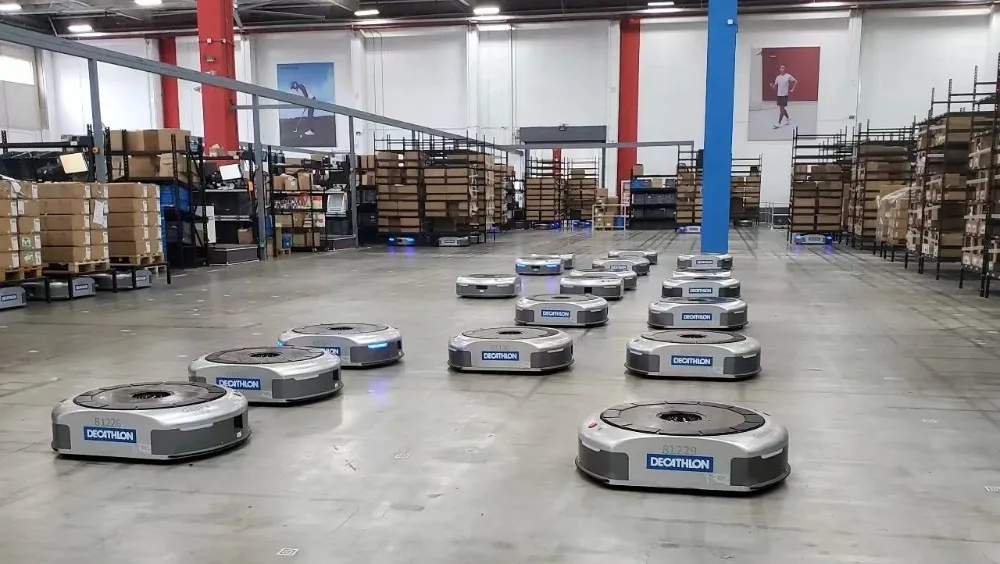
1,000+ robots deployed in a single warehouse for global sporting goods leader
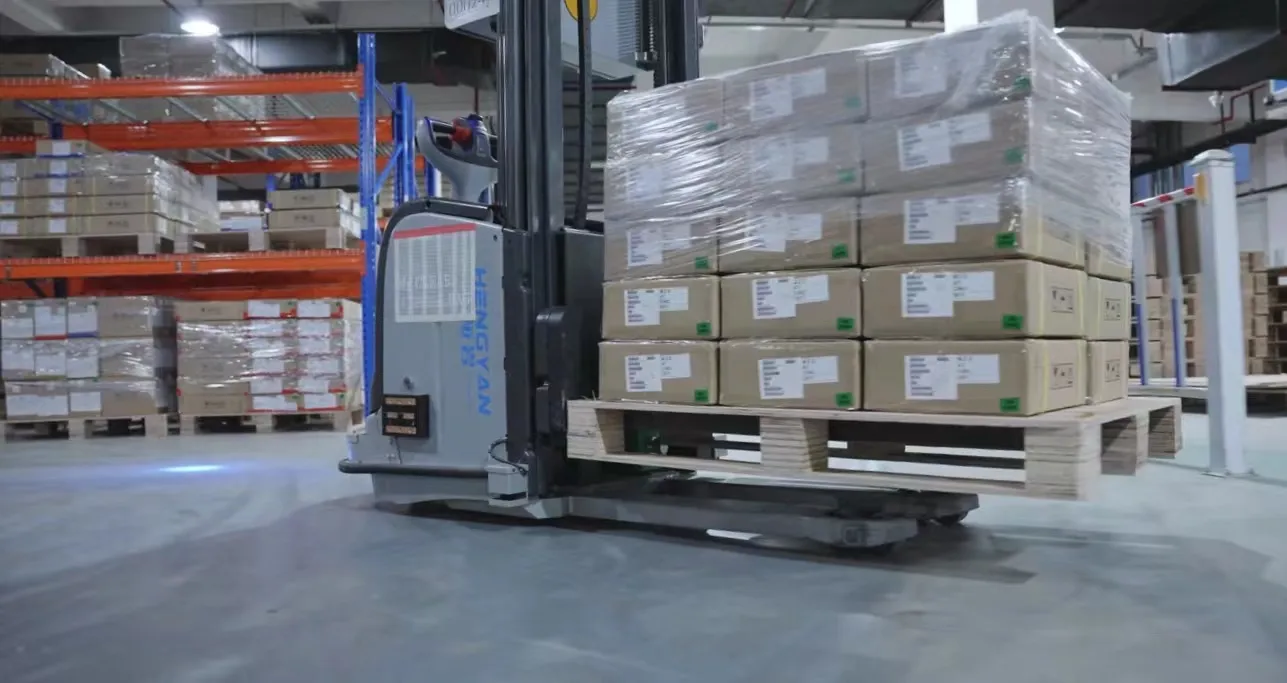
Laser SLAM forklift AGV + ERP integration: 24/7 automated logistics for high-mix PCB production
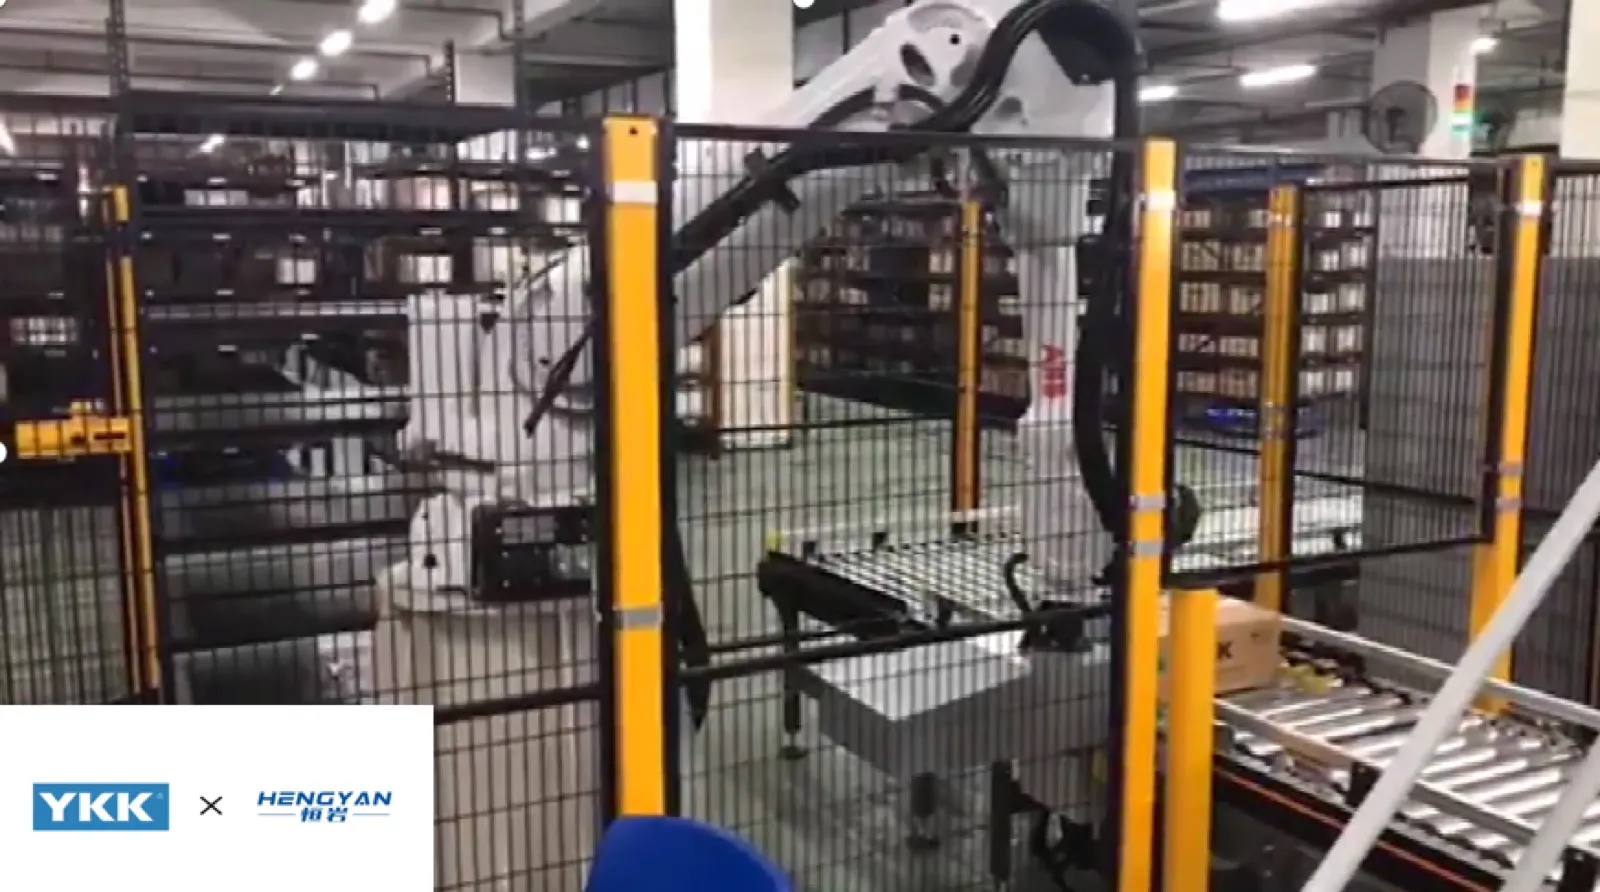
Bin robots + robotic arm: a benchmark for fully automated case-level storage and picking
Tell us about your warehouse challenges — our team will design a tailored automation plan for you.